If you’ve ever held a can of soda, run your hand over a car door panel, or even grabbed a steel wrench, you’ve interacted with a product that went through hot rolling. As a hot rolling equipment supplier, I get asked this question all the time: “What’s the actual principle behind this process, anyway? It sounds super industrial—how does it work?” Let’s break it down like I’m explaining it to a buddy who’s not a steel engineer, no stuffy jargon, no confusing equations, just real, straight talk. Hot Rolling Equipment
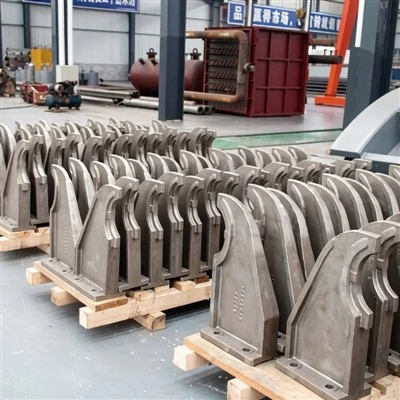
First, let’s set the scene. Hot rolling isn’t something you do to cold, hard steel you just picked up from a hardware store. Those big blocks we start with? They’re called ingots, or sometimes billets if they’re smaller. Before they even hit our rolling equipment, they spend hours in a furnace—think a really, really intense oven, like 1100 to 1300 degrees Celsius hot. That’s way hotter than molten candle wax, hot enough that steel stops being that rigid, snap-easily stuff and turns soft and malleable. That temperature is key here. See, metals have what’s called a recrystallization temperature, right? For steel, that’s roughly 727 degrees Celsius. Hot rolling happens way above that mark—so every time we squeeze the metal between the rollers, it doesn’t work-harden and crack like cold steel would. Instead, the new grains that form are tiny, uniform, and strong, not brittle. That’s the big principle right there: work the metal when it’s soft, above its recrystallization temp, to shape it into the exact size and shape you need.
Wait, let’s make that relatable. If you’ve ever tried to bend a cold paperclip, it snaps if you push too hard. But if you heat the end of that paperclip over a flame until it’s glowing orange, suddenly you can bend it into a hook without breaking. That’s exactly what hot rolling does, just on a massive scale. Our equipment isn’t a flame and a paperclip; it’s a series of heavy, rotating rollers—some big as a truck tire, some even bigger—mounted in a sturdy frame, connected to huge motors that crank out thousands of horsepower. When the soft, hot billet or slab feeds between two rollers, the gap between them is set just slightly smaller than the metal’s current thickness. The rollers grip the metal, pull it through, and squeeze it down. But here’s the trick: we don’t do that in one step. If you tried to squash a 10-inch thick steel slab down to 1 inch in one pass, you’d either break the rollers or the metal would crack. So we do it in stages, with multiple stands of rollers lined up in a row. Each stand takes a small bite—maybe reducing the thickness by 10 to 20%—until we get to the final size. That incremental reduction is another core principle: gradual deformation to control the metal’s shape and quality, instead of forcing it all at once.
Now, let’s talk about why that gradual step matters more than you might think. Every time the metal passes through a roller stand, we can also adjust its width, not just its thickness. If you want a long, flat steel sheet for roofing, we can make the rollers slightly angled so the metal spreads evenly as it’s squeezed. If you need a round bar for building, we use grooved rollers that shape the soft metal into a circle as it’s pulled through. But it’s not just about size—we’re also controlling the metal’s internal structure. Those big ingots from the mill have imperfections, right? Tiny voids or uneven grains from when they cooled. Hot rolling, done right, closes those voids and aligns the grains in the direction the metal is being rolled. That makes the final product way stronger than the original ingot. I’ve had a customer come to me before saying, “We used to buy cold-rolled bars and they’d snap during bending—then we switched to your hot-rolled ones and now they hold up for years.” That’s the principle in action: shaping and strengthening in one step, because the heat lets us work the metal without ruining its integrity.
Wait, let’s address a common misconception: people think hot rolling is just heating metal and rolling it, but there’s way more to it than that. Our equipment has temperature control systems that keep the metal consistent the entire time it’s being rolled. If a section cools too much mid-process, it might drop below recrystallization temp, turn hard, and crack—so we have induction heaters or convection hoods along the line to top up the heat. We also have sensors that measure thickness, width, and even flatness every fraction of a second, adjusting the roller gaps in real time. Last year, a customer was having trouble with their sheets curling at the edges after rolling; we modified the roller alignment on our equipment to apply slightly more pressure on the edges, and that fixed the problem. That’s not just “running rollers”—that’s applying the principle of controlled, uniform deformation to avoid defects.
Another key part of the principle here is friction, believe it or not. The rollers can’t just push the metal; they have to grip it to pull it through. If the friction is too low, the rollers spin but the metal doesn’t move. If it’s too high, the metal could get scratched or torn. That’s why we often use a light lubricant, like water-based oil, on the rollers—not to cool them down (we have separate cooling systems for that), but to get just the right amount of grip. It’s a fine balance, and it’s something our equipment is calibrated to get right every single time, no matter what type of steel or alloy we’re working with.
Let’s also talk about what happens after the rolling, because that ties back to the core principle. Once the metal is the size and shape we want, it’s still hot—like 500 degrees or more. If we let it cool randomly, it might warp or develop uneven stresses. So we use laminar cooling systems: rows of water jets that spray controlled amounts of water across the metal as it moves on a conveyor. That cools it evenly, locking in the shape and the grain structure we created during hot rolling. It’s like taking a hot pizza out of the oven and letting it cool on a stone instead of a flimsy plate—you want it to stay the way you shaped it, not bend or crack.
Now, why does this all matter to you? If you’re in manufacturing—whether you make cars, appliances, construction materials, or even aerospace parts—hot rolling is the first step to most of your raw materials. The quality of your final product starts with how that hot rolling is done. If the equipment is mis calibrated, or the temperature is off, you’ll end up with defects that mean wasted materials, delayed production, or products that don’t meet safety standards. That’s where we come in. As a hot rolling equipment supplier, we don’t just sell you a bunch of big rollers. We design our equipment around that core principle: work metal above recrystallization temp, control deformation incrementally, maintain consistent heat and friction, and adjust in real time to avoid defects. We’ve spent years tweaking our systems to handle everything from mild steel to high-strength alloys, so our customers don’t have to waste time troubleshooting problems that could have been avoided with the right equipment.
I get it, industrial equipment can feel overwhelming if you’re not deep in the steel world. But the principle is simple, even if the hardware to execute it is complex. It’s the same idea as shaping clay on a pottery wheel—you work it when it’s soft, not when it’s dry and brittle, to get the shape you want, and it turns out way stronger. Hot rolling is just that, but for metals at 1000 degrees, with machinery that can lift thousands of tons.
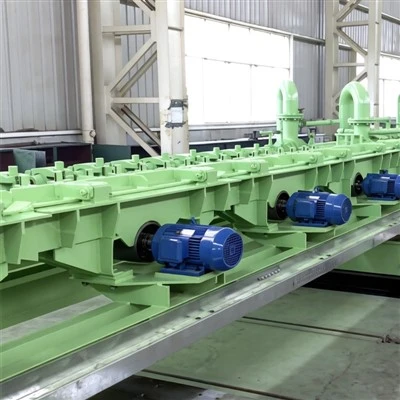
If you’re looking to upgrade your hot rolling line, troubleshoot a production issue, or just learn more about how our equipment can help you make better products, feel free to reach out. We can walk you through the specifics, answer any questions, and help you find the right setup for your needs.
Heating Furnace References
Manufacturing Processes for Engineering Materials, Kalpakjian S. and Schmid S.R.
Rolling Theory and Practice, Iron and Steel Society.
Modern Hot Rolling Technology, Association for Iron and Steel Technology.
Jiangsu Dongfang Whole-Set Equipment Manufacturing Group Co., Ltd.
We are one of the most professional hot rolling equipment manufacturers and suppliers in China, also support customized service. With abundant experience, we warmly welcome you to buy durable hot rolling equipment from our factory. If you have any enquiry about pricelist, please feel free to email us.
Address: No. 9, Industrial Park, Xinqiao Town, Jingjiang City, Jiangsu Province
E-mail: dfctwm@163.com
WebSite: https://www.dongfangequip.com/
